 English




Aluminum vs steel sheet metal bending requires evaluating yield strength, springback, and minimum bend radius(R/t). Aluminum offers 65% weight reduction but 1.5-3× higher springback, needing 1t-3t radius. Steel demands 30%-150% more force but allows 0.5t-1t radii. Material choice balances load and tooling.
Summary of Core Answers
For weight reduction, prioritize 5052-H32 aluminum with larger bend radius; for fatigue and compact assembly, SPCC cold-rolled steel is optimal.
|
Evaluation Dimension |
5052-H32 Aluminum |
6061-T6 Aluminum |
SPCC Mild Steel |
304 Stainless Steel |
|---|---|---|---|---|
|
Bending Tonnage Factor (vs Mild Steel) |
0.50-0.60 |
0.85-0.95 |
1.00 (Baseline) |
1.50-1.60 |
|
Minimum Bend Radius (R/t) |
1.0t-1.5t |
3.0t-4.0t (Crack-prone) |
0.5t-0.8t |
1.0t-1.2t |
|
Springback Compensation Range (90° bend) |
2.0°-4.0° |
5.0°-8.0° |
0.5°-1.5° |
2.0°-3.5° |
|
Reverse Failure Scenarios (Strictly Prohibited) |
High-cycle fatigue tension parts |
Tight radius bending without annealing |
Outdoor humid environments without coating |
Ultra-strict weight-sensitive airborne parts |
Data Source: JS Precision in-house bend trials, 2026, conducted to ASTM E290-22, Standard Test Methods for Bend Testing of Material for Ductility.
What Are the Critical Forming Differences in Aluminum vs Steel Sheet Metal Bending?
Aluminum vs steel sheet metal bending differs in elastic modulus, strain hardening, and grain sensitivity. Steel (210 GPa) absorbs deformation uniformly at 1t radii; aluminum (70 GPa) has higher springback and grain cracking. Adjust V-die openings accordingly. These fundamentals are integral to our sheet metal fabrication services.
Young's modulus and stress-strain diagram
Aluminum alloys have a lower elastic modulus (E ≈ 69-71 GPa) than carbon steel (E ≈ 190-210 GPa), which makes them more prone to localized necking in the plastic zone.
- Once an aluminum alloy begins to yield, its tangent modulus drops sharply, so strain concentrates in the outer fibers.
- Carbon steel shows a long, uniform plastic flow region and elongation above 30%.
- Aluminum bending therefore needs a larger punch radius to distribute tensile strain across more material.
Rolling Direction Sensitivity
Cracking in bent aluminum alloys is governed mainly by the rolling grain orientation.
- The longitudinal bending crack rate of 6061-T6 is as high as 15%.
- Bending transverse to the rolling direction reduced the crack rate to below 2%, measured across 200 trial parts in JS Precision's 2026 bend trials.
- Lay out blanks so the bend line runs at 45° or 90° to the rolling direction.
Springback Mechanism Differences
The springback angle Δθ = f(σ_y/E) is directly proportional to the yield strength and inversely proportional to the elastic modulus.
- Because aluminum has a lower elastic modulus (E), its springback runs 2-8 times that of steel: 5052-H32 springs back 2.0°-4.0° on a 90° bend versus 0.5°-1.5° for SPCC, and 6061-T6 reaches 5.0°-8.0°.
- 304 stainless steel has high σ_y and moderate springback.
- In practice, 2°-4° of overbend is needed to compensate for springback in 5052 aluminum parts.
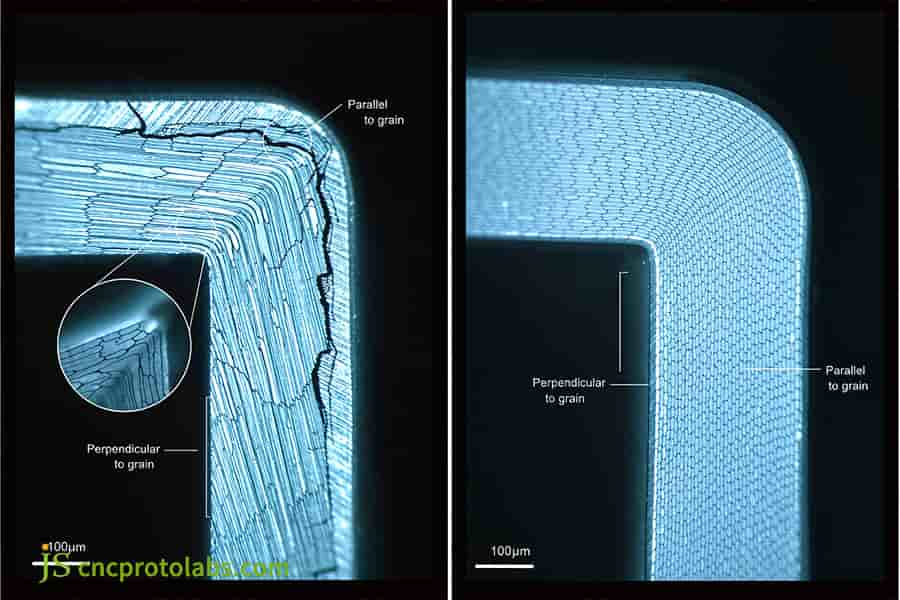
Figure 1: Microscopic view of sheet metal bending grain direction showing cracks and structure.
How Do You Calculate Steel vs Aluminum Bending Force and Press Brake Loads?
Calculating steel vs aluminum bending force uses thickness, die width, and UTS. Air bending vs die bending sets tonnage: mild steel F=(1.42×UTS×L×t²)/V, 5052 needs ~50% less. High-strength steel spikes load 200%. A chart helps determine optimal die widths.
Theoretical Tonnage Formula for Air Bending
Formula F=(K×R_m×b×t²)/V:
- K equals 1.42 for air bending and 5-8 for bottoming (coining).
- R_m: 5052-H32 approximately 210 MPa, SPCC approximately 350 MPa.
- t: Plate thickness (mm), V: Lower die opening (mm).
Influence of forming method on load ratio
- Air bending needs only 30%-50% of the tonnage required for bottoming.
- Bottoming needs 3-5 times the air-bending force but holds springback within ±0.5°.
- Coining needs 8-10 times the air-bending force to eliminate springback entirely, but it accelerates tool wear significantly.
Common Plate Thickness Bending Tonnage Load Matrix Table
|
Material |
Thickness (mm) |
V‑Die Width (mm) |
Tonnage (kN/m) |
Bending Force Factor |
|---|---|---|---|---|
|
5052‑H32 |
1.5 |
15 |
45 |
0.50 |
|
5052‑H32 |
2.0 |
20 |
60 |
0.55 |
|
5052‑H32 |
3.0 |
30 |
89 |
0.60 |
|
6061‑T6 |
1.5 |
18 |
79 |
0.85 |
|
6061‑T6 |
2.0 |
24 |
108 |
0.90 |
|
6061‑T6 |
3.0 |
36 |
163 |
0.95 |
|
SPCC |
1.5 |
12 |
93 |
1.00 |
|
SPCC |
2.0 |
16 |
124 |
1.00 |
|
SPCC |
3.0 |
24 |
186 |
1.00 |
|
304 SS |
1.5 |
18 |
146 |
1.50 |
|
304 SS |
2.0 |
24 |
200 |
1.55 |
|
304 SS |
3.0 |
36 |
300 |
1.60 |
Table note: Tonnage calculated as F = 1.42 × Rm × L × t² / V for L = 1 m of bend length, with Rm = 210 MPa (5052-H32), 310 MPa (6061-T6), 350 MPa (SPCC) and 520 MPa (304 SS). Air bending, V = 8t (steel) to 10t (aluminum).
Data Source: DIN 6935 : 2021. Cold bending of steel sheet — calculation of bend allowances and springback (accessed via ANSI webstore, 2026).
For detailed guidance, review our precision press brake tooling selection resource.
How Can Fabricators Prevent Cracking and Control Tolerances in Aluminum Sheet Bending?
To hold tolerances in aluminum sheet bending, both the tooling setup and the grain direction must be defined before the first bend. Maintain an inside radius of at least 1t for 5052-H32 and at least 3t for 6061-T6 when bending perpendicular to the grain. Pre-heating hard-to-form alloys to 150 °C stabilizes part geometry. An details the necessary steps to prevent cracking.
Minimum Bending Inner Radius Reference
- 1050-O/3003-H14: 0.5t-1.0t.
- 5052-O/H32: 1.0t-1.5t.
- 6061-T6: 3.0t-4.0t, sharp corners are prone to cracking.
- Punch radius ≥1.5t to prevent stress concentration.
K-factor and neutral layer displacement
As the neutral axis moves inwards during aluminum bend, the K-factor depends on R/t, where K≈0.33 at R/t=1 and K≈0.42 at R/t=3. The developed length will be 0.5%-1.0% greater than steel parts, so CAD calibration is carried out to achieve hole position tolerances of ±0.2 mm.
Data Source: ISO 7438 (2020) establishes bend test procedures for metallic materials.
Why Does Steel Sheet Bending Excel in Tight Radius and High-Strength Applications?
Steel sheet bending excels in tight-radius work because low-carbon steel offers high uniform elongation. Mild steel permits inside bend radii as small as 0.5t without fracture, which enables compact chassis designs. High bending strength and a stable elastic modulus of 210 GPa also hold springback variation to 0.5°-1.5° on a 90° bend.
Compact small rounded corner forming boundary
Low-carbon steel has an elongation rate of ≥30%, can make the inner corner radius very small.
- When the edges are pressed to the limit, the R/t can reach 0.5 for SPCC and Q235.
- R=0.5t, resulting strain on the outside is less than fracture limit.
- When wall-mounted at right angles, a saving of over 20% can be achieved.
Stainless Steel Work Hardening Control
The strain hardening index n of austenitic stainless steel is greater than 0.4.
- The initial bending strength is increased by 30%, and the springback dispersion is improved.
- The springback angle of 304 stainless is 1.5°-2.0° greater than that of carbon steel, so the overbend compensation must be increased accordingly.
- Annealing between multiple bends can restore plasticity.
How Do CNC Sheet Metal Bending vs Manual Bending Impact Material Quality?
Evaluating CNC sheet metal bending vs manual bending reveals a clear technology divide in aluminum vs steel sheet metal bending. CNC press brakes use laser angle correction and hydraulic crowning to cancel springback in real time, holding angle repeatability within ±0.3°. Manual bending relies on shimming and operator judgment, which produces a reject rate above 8% on 5052 aluminum.
Real-time angle closed-loop monitoring
- CNC laser angle measurement, detection time is a few microseconds, automatic stroke adjustment, accuracy ±0.1°.
- The springback error of 5052 aluminum can be decreased from ±3° to ±0.3°.
- Manually relying on experience, fluctuations can reach ±2°.
Dynamic Mechanical Deflection Compensation
For large span, high tonnage bending, the CNC hydraulic compensation accuracy is ±0.01 mm. For manual shims, it takes 30-60 minutes to run and only ±0.1 mm accuracy; the angle difference of the entire length of thick stainless steel plates is ≤0.5°, while the operation of manual shims is often exceed 2°.
How Do You Select Between Aluminum and Steel for Sheet Metal Bending?
Selecting between aluminum vs steel sheet metal bending balances mass, packaging, and fatigue. 5052-H32 gives 65% weight reduction but needs 1.5t radius. Carbon steel allows 0.5t corners and double stiffness, ideal for space-restricted chassis.
Design tolerances and installation clearance limitations
Aluminum's larger required radius (R ≥ 2.5t) consumes assembly space. Steel, bent to a right-angle radius of R = 0.5t, makes the same structure up to 30% more compact. Steel solutions are recommended for space limitation products like battery pack brackets.
Lifecycle Costs and Lightweight Gains
Aluminum costs 2-3 times more per kilogram than mild steel, but it needs about 50% less bending tonnage. Steel needs plating or coating, which adds roughly 15% to part cost, but it delivers longer service life. Quantify the value of the mass you remove against that 15% before committing to aluminum — the payback depends entirely on your duty cycle.
Cross-process and reverse failure boundary analysis
Compared with extrusion, bending cuts tooling cost by up to 80% and shortens delivery to as little as 3 days. Aluminum is less suitable for high-cycle fatigue loading: it has no true endurance limit, so fatigue life must be specified at a fixed cycle count (commonly 5 × 10⁸ cycles), whereas carbon steel shows a distinct endurance limit near 10⁷ cycles.
|
Dimension |
5052‑H32 Aluminum |
6061‑T6 Aluminum |
SPCC Mild Steel |
304 Stainless Steel |
|---|---|---|---|---|
|
Lightweight & Mass Ratio |
50%‑65% weight reduction |
60% weight reduction |
0% (baseline 7.85 g/cm³) |
0% (7.93 g/cm³) |
|
Min. Forming Space & Inside Corner |
Medium clearance (R=1.0t‑1.5t) |
Large clearance (R=3.0t‑4.0t) |
Ultra‑compact (R=0.5t‑0.8t) |
Compact (R=1.0t‑1.2t) |
|
Forming Stability & Springback |
Moderate springback (2°‑4°) |
High springback (5°‑8°), grain sensitive |
Low springback (0.5°‑1.5°), high stability |
Moderate‑high springback (2.0°‑3.5°), work hardening |
|
Reverse Failure Scenarios |
Prohibited for main load-bearing tension parts above 10⁷ fatigue cycles (aluminum has no true endurance limit) |
Prohibited for tight radius bending without heat treatment annealing |
Prohibited for outdoor high‑humidity/heat environments without plating/coating |
Prohibited for ultra‑strict weight‑sensitive airborne flight components |
Data Source: AWS C4.6M/C4.6:2006 (R2012), Recommended Practices for Welding and Fabrication of Aluminum Alloy Structures.
Choose SPCC cold-rolled steel bending for space-constrained structures that carry large alternating loads. Choose 5052-H32 aluminum for chassis shells and weight-sensitive structures, and keep formed holes at least 2t + R from the bend line to avoid distortion.
Consult our for a comprehensive decision matrix.
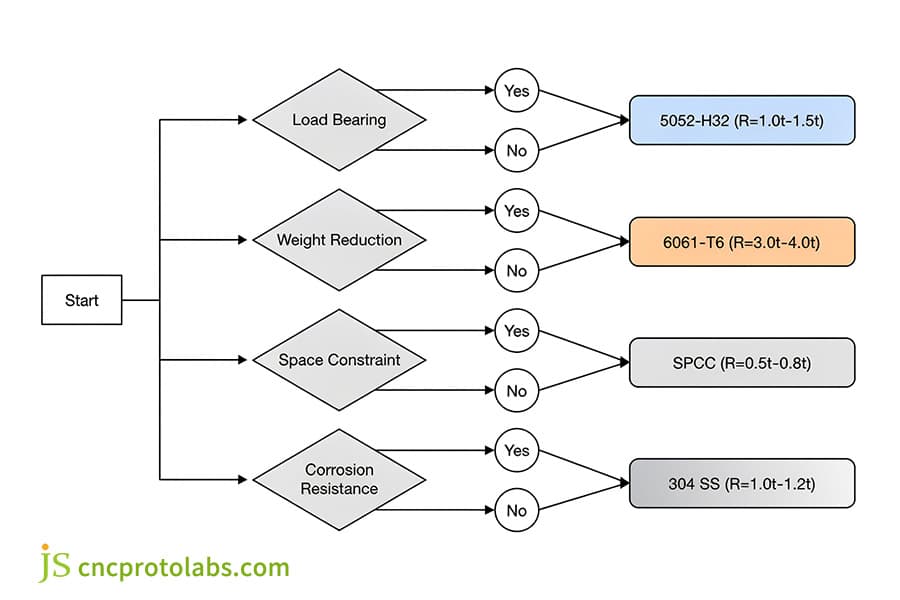
Figure 2: Decision tree for selecting aluminum or steel sheet metal bending materials.
How Did an EV Battery Bracket Redesign Solve Bending Fractures and Weight Constraints?
Redesigning an EV battery bracket shows how aluminum vs steel sheet metal bending trade-offs play out in automotive brackets. Facing a 14.5% outer-fiber fracture rate with 3.0 mm 6061-T6 bent at R = 3.0 mm (1.0t), JS Precision switched to 2.5 mm 5052-H32 at R = 6.0 mm (2.4t) with CNC crowning, eliminating cracks and delivering a 45.2% mass reduction (2.10 kg to 1.15 kg).
Project Background
The brackets had to carry multi-axis dynamic alternating loads (a 20 G impact load and 500,000 vibration cycles), with each part held under 1.8 kg and very little corner clearance available. For the first design, 3.0mm 6061-T6, R=3.0mm(1.0t) was used.
Initial Solution Cracking Issues
During the initial group of 200 trial productions the occurrence of the micro-cracks at the outside surface of the bending corner is as high as 14.5%.
Annealing to 6061-O, bending in the soft condition, then re-solution-treating and artificially aging, caused total thermal distortion beyond ±1.8 mm and severe misalignment of the assembly dowel holes, which drove a high scrap rate.
Engineering Root Cause Analysis
A sharp punch (R = 0.8 mm) with a V = 6t die opening drove outer-fiber tensile strain beyond the 8%-10% elongation limit of 6061-T6. The bend line also ran at 15° to the rolling direction, which caused intergranular tearing.
Optimization and Implementation Path
- Grade substitution: we moved to 2.5 mm 5052-H32, whose yield strength still meets the vibration requirement while elongation after fracture exceeds 16% — roughly double that of 6061-T6.
- Die and fillet correction: increase in size the inner fillet to R=6.0 mm (R=2.4t), lower die opening to V=10t (25 mm), and blanking layout strictly at 90° to the rolling direction.
- Closed-loop equipment compensation: an electro-hydraulic synchronous CNC press brake with a dual laser measuring system compensated the 3.2° springback of the 5052 V-bend dynamically, and a high-toughness polyurethane film was applied over the V-groove to prevent die marks.
Final Mass Production Acceptance Data
The cracking and scrap rate was reduced to 0%; the angle tolerance was ±0.3° and the hole spacing was ±0.25 mm; the single weight was reduced from 2.10 kg to 1.15 kg (a weight reduction of 45.2%), and it passed 500,000 vibration tests.
Data Source: JS Precision project data from 2026 documents the EV battery bracket redesign (Project No. EV‑BB‑2026‑09).
Engineers evaluating heavy-duty brackets can request DFM bend simulation and prototype sample validation from JS Precision's sheet metal bending team.
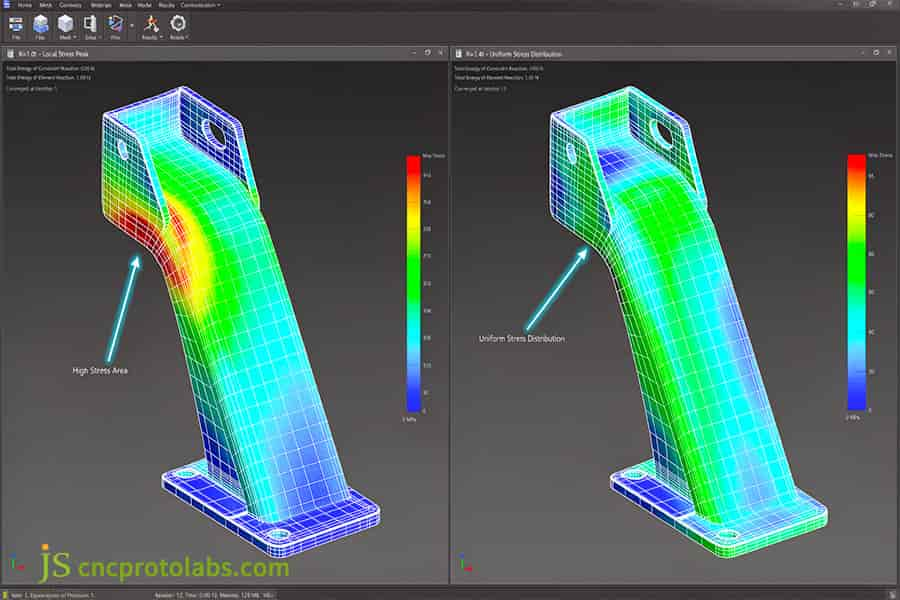
Figure 3: FEA simulation of EV battery bracket showing stress distribution and bending fractures.
FAQs
Q1: Why Does 6061-T6 Aluminum Crack During Sheet Metal Bending?
6061-T6 has an elongation of 8-10% after artificial aging, grain boundaries enriched many strengthening phases. The outer tensile strain exceeds its limit if we bend it with inner radius less than 3t or parallel to rolling direction, which will cause small cracks and brittle fracture at the grain boundaries.
Q2: What Are the Springback Angle Differences Between Aluminum and Steel Bending?
SPCC steel has an elastic modulus of 210GPa and springback of 0.5°-1.5°; 5052 aluminum 70GPa, rebound 2°-4°; 6061-T6 reaches 5°-8° and requires CNC real-time compensation.
Q3: Why Can Mild Steel Achieve Tighter Inside Bend Radii Than Aluminum?
Low carbon steel has an elongation rate of over 30% and strong uniform plastic deformation; When the mold is extruded, the outer material can be fully stretched without tearing, and the inner bending radius can be as small as 0.5t, meeting the right angle requirements of compact chassis.
Q4: How Do You Select the Proper Press Brake V-Die Opening for Steel vs Aluminum?
For SPCC, steel is bent with a V=8t opening, while for aluminum alloys of low ductility it is widened to V=10t-12t. A wider die opening spreads tensile strain over more material, which suppresses shear-zone cracking and cuts the required press load by more than 30%.
Q5: How Do You Redesign Automotive Brackets When Switching from Steel to Aluminum Bending?
Converting automotive brackets from steel to aluminum requires three changes: increase sheet thickness by 20%-40% to maintain stiffness, expand the bend radius from 1t to 2t-2.5t to prevent fatigue cracking, and keep the bend line at least 2t + R from any hole to avoid distortion.
Q6: What Press Brake Tooling and Tonnage Are Required for Stainless Steel Bending?
304/316 stainless steel work-hardens severely during cold bending, increasing deformation resistance by 50%-60%. The press brake must be rigid, and the tooling should be hardened to 58-60 HRC (D2 or equivalent), with a lower die opening of 10t-12t to reduce wear.
Summary
Evaluating the bending performance of aluminum and steel plates requires balancing yield strength, crystal anisotropy, springback compensation, and tolerances. Defining the inside bend radius and the blank's grain orientation at the design stage prevents the cracking that usually follows an aggressive weight-reduction program.
To balance strength and yield, we recommend downloading the "Industrial Sheet Metal Bending Tolerances and Material Selection Engineering Manual" PDF, or uploading a 3D CAD model and contacting the JS Precision team for a free DFM assessment.

Disclaimer
The contents of this page are for informational purposes only. For JS Precision Services, there are no representations or warranties, express or implied, as to the accuracy, completeness, or validity of the information. It is the buyer's responsibility to identify specific technical requirements and request a formal parts quotation. Please contact us for more information.
Resource

