 English




Carbon steel laser cutting service assists in gas selection, directly determining cut quality and cost by matching oxygen, nitrogen, or compressed air to material thickness. Use 0.6–2.5 bar industrial oxygen for carbon steel ≥ 6 mm; 14–22 bar high-purity nitrogen for thin carbon steel and for stainless steel whenever you need an oxide-free, bright edge; and clean compressed air at 14–16 bar for low-carbon steel up to 3 mm, where it removes about 75% of the hourly gas cost.
Core Answer Summary Table: Laser Cutting Gas Selection
|
Material & Thickness Range |
Recommended Assist Gas |
Pressure Setting (bar) |
Edge Roughness (Ra) |
Post-Process Compatibility |
|---|---|---|---|---|
|
Mild Steel Thick Plate (≥ 6 mm) |
Industrial Oxygen (O2) |
0.6–2.5 bar |
Ra 6.3–12.5 μm — with oxide scale present |
Requires oxide removal, suitable for heavy welding |
|
Mild Steel Thin Plate (0.5–4 mm) |
High-Pressure Nitrogen (N2) |
14–18 bar |
Ra 1.6–3.2 μm — silver-white, dross-free |
Powder coating without secondary grinding |
|
Austenitic Stainless Steel (Full Thickness) |
High-Purity Nitrogen (≥ 99.999%) |
16–22 bar |
Ra 0.8–1.6 μm — mirror-bright, no heat tint |
Preserves passivation layer, direct TIG welding |
|
Structural Carbon Steel (1–3 mm) |
Clean Compressed Air |
14–16 bar |
Ra 3.2–6.3 μm — slight oxidation |
Indoor powder coating and mechanical assembly |
Data source: JS Precision internal production records, Jan–Dec 2025: 148 laser cutting jobs on 6 kW and 12 kW fiber lasers across 0.5–16 mm carbon steel and 0.5–12 mm stainless. Roughness was measured by contact profilometer (cut-off 0.8 mm, ISO 4288); values shown are the measured range across the job set, not catalogue figures. The same dataset backs the case study and FAQ numbers in this article.
Carbonsteel is making use of an exothermic oxygen reaction and this way is reducing energy consumption. Then again, parts of stainless steel with high surface quality requirements, as well as certain carbon steel parts, need to be treated with high-pressure nitrogen for physical slag removal and oxidation prevention.
Why Do Assist Gases React Differently in Carbon Steel vs Stainless Laser Cutting?
In carbon steel vs stainless laser cutting, assist gas dynamics dictate whether kerf evacuation relies on exothermic combustion or supersonic inert expulsion. Low-pressure oxygen at 0.6 to 2.5 bar generates an iron-oxidation reaction that supplies 55% to 65% of the total cutting energy on carbon plates. Conversely, laser cutting gas selection for stainless steel utilizes non-reactive nitrogen at 16 to 22 bar to physically eject molten chromium-rich dross without surface oxidation.
Oxidation exothermic equation for oxygen-assisted melting of carbon steel and low-pressure temperature control logic
- When oxygen is used as a fuel for the melting of carbon steel the heat produced by the ferro-oxygen reaction contributes up to 55–65% of the cutting energy. Still, if the gas pressure goes beyond 2.5 bar then the overheating of the molten pool will cause the cut to become uncontrolled and result in defects like melt sinking.
- The laser cutting gas selection is such that the nozzle height can be controlled between 0.5 and 1.0 mm which will keep the molten pool stable and prevent heat accumulation at the corners of thick plates.
Physical properties of molten stainless steel and supersonic nitrogen slag removal mechanism
- Molten stainless steel carries chromium and nickel, which raise its viscosity and reduce its fluidity compared with molten carbon steel. Because the thick melt does not drain cleanly from the kerf, it re-solidifies on the lower cut edge and forms hard dross — which is exactly what high-pressure nitrogen has to eject.
- To clear both the dross and the heat tint, you need a genuinely supersonic coaxial jet: nitrogen at 16–22 bar delivered through a 0.15–0.30 mm annular gap. The jet develops enough dynamic pressure to overcome the surface tension of the molten metal and scrub the full kerf wall, so both the slag and the heat tint leave with the exhaust stream.
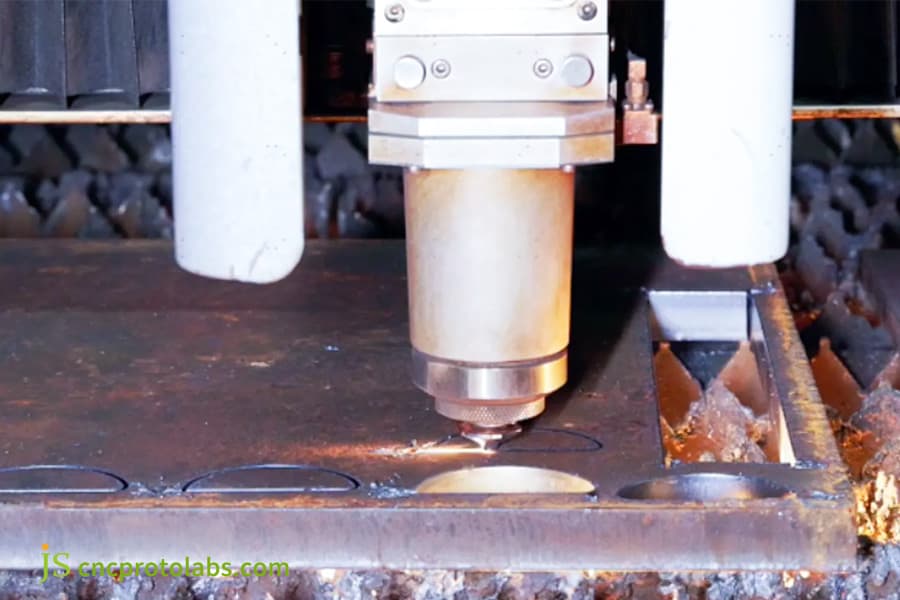
Figure 1: Fiber laser head cutting 12 mm carbon steel plate with low-pressure oxygen assist; note the characteristic spark plume of reactive cutting.
Oxygen vs Nitrogen Laser Cutting for Mild Steel: Where Is the Thickness Cutoff?
In mild steel laser cutting, the process shift for oxygen vs nitrogen laser cutting centers on a 4 to 6 mm thickness cutoff. Sheets below 4 mm utilize 14 to 18 bar nitrogen to secure oxide-free Ra 1.6 to 3.2 μm edges for immediate coating powder. Beyond 6 mm, industrial laser cutting carbon steel requires 0.6 to 2.5 bar oxygen to prevent prohibitive gas consumption exceeding 60 Nm³/h.
Oxygen cutting process window and oxide layer characteristics
- The residual brittle iron oxide layer on the oxygen cutting section is 0.05-0.2 mm, with a surface roughness of Ra 6.3–12.5 μm, suitable for ordinary heavy industry welding and rough machining.
- For the laser cutting process of mild steel, holding pressure precisely between 0.6 and 2.5 bar balances cutting energy against cross-sectional quality: below 0.6 bar the reaction front starves, and above 2.5 bar the melt pool overheats and the kerf loses control.
High-pressure nitrogen cutting gas consumption and process switching boundary
- If the carbon steel sheet thickness is increased, more than 6 mm, the nitrogen consumption by high-pressure cutting will go up drastically. 10 mm carbon steel gas consumption will reach about 60–80 Nm³/h only. Meanwhile, energy consumption will also grow very rapidly, which will result in the costs being out of control.
- In the range of the 4–6 mm sheet thickness, engineers should specify the clear process changing limits given the sheet thickness: less than 4 mm nitrogen is used to get cuts without oxides, over 6 mm oxygen is turned to benefit from an exothermic reaction this way saving gas.
Comparison Table of Low Carbon Steel Plate Thickness vs. Gas Selection Process Parameters
|
Sheet Thickness (mm) |
Recommended Gas |
Nozzle Diameter (mm) |
Pressure (bar) |
Cutting Speed (m/min) |
Surface Roughness (Ra) |
|---|---|---|---|---|---|
|
0.5–3 |
Nitrogen (N2) |
1.5 |
14–18 |
2.5–4.0 |
Ra 1.6–3.2 μm |
|
4–6 |
Nitrogen / Oxygen |
1.5–2.0 |
14–18 / 0.6–1.5 |
1.5–3.0 |
Ra 3.2–6.3 μm |
|
8–10 |
Oxygen (O2) |
2.0 |
1.5–2.5 |
0.8–1.5 |
Ra 6.3–12.5 μm |
|
12–16 |
Oxygen (O2) |
2.0–2.5 |
2.0–2.5 |
0.5–0.8 |
Ra 12.5–25 μm |
ISO 9013:2017, Thermal cutting — Classification of thermal cuts — Geometrical product specification and quality tolerances, defines the perpendicularity (u) and roughness (Rz5) tolerance grades that apply to laser-cut carbon steel. It is the tolerance basis for the thickness/parameter table below.
According to JS Precision 2025 project data, gas consumption and edge roughness measurements for mild steel cutting under various assist gases.
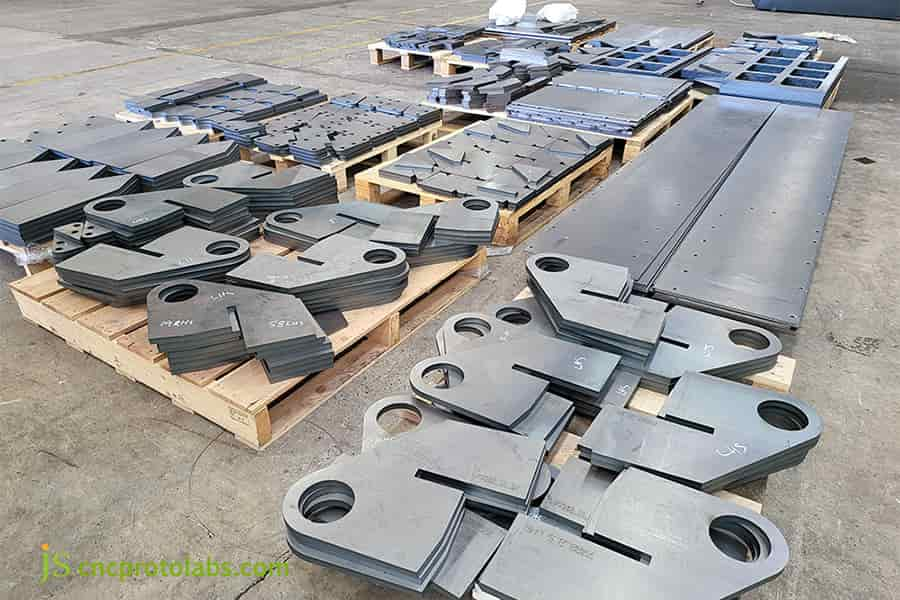
Figure 2: Palletised mild steel blanks after nitrogen cutting — bright, oxide-free edges with no secondary grinding.
Why Must Stainless Steel Laser Cutting Service Demand High-Purity Nitrogen?
Stainless steel laser cutting service mandates grade 5.0 nitrogen (≥ 99.999% purity) at 16 to 22 bar to stop molten chromium from volatilizing into brittle oxides. During laser cutting gas selection, gas purity slipping below 99.99% destroys the native passivation layer defined by ASTM A380.This contamination causes cut-face yellowing and degrades ASTM B117 salt spray corrosion resistance by over 60% without mechanical decontamination.
The Influence Mechanism of Gas Purity on Corrosion Resistance and Metallographic Structure of Metal Cross Sections
- Cutting with nitrogen at ≥ 99.999% purity and 16–22 bar leaves a smooth, silvery-white cut face with no heat tint. The surface is weld-ready: no chemical pickling is needed before robotic argon arc welding process, which removes an entire process step — and its waste stream — from the routing.
- The selection of laser cutting gas is very important. A tiny leak in the gas delivery system introducing a mere 0.05% impurity from the air will decrease the life of stainless steel sections as determined under a salt spray resistance test from 240 h to <48 h.
Expansion characteristics of high-pressure gas inside the nozzle and selection of double-layer coaxial nozzles
- High-pressure gas inside the nozzle performs adiabatic expansion causing the formation of a supersonic core flow. The double-layer coaxial nozzle concept, in addition, well retains the airflow beam shape focusing and stops pressure loss caused by airflow divergence.
- When the nozzle orifice diameter (1.5–2.0 mm) is accurately fitted to the air pressure (16–22 bar), the resulting supersonic dynamic pressure is sufficient to break up the surface tension of the molten metal, and as a result, the slags and burrs at the bottom edge of the stainless steel cuts can be fully eliminated.
ASTM A380/A380M-17, Standard Practice for Cleaning, Descaling, and Passivation of Stainless Steel Parts, sets the passivation requirement referenced by the nitrogen-cut edge condition above. (Verify the current edition in the ASTM catalog before publishing — the -17 edition may have been superseded.)
ASTM B117, Standard Practice for Operating Salt Spray (Fog) Apparatus, is the corrosion test method behind the 240 h versus <48 h figures quoted above. Test data source: JS Precision internal production records, 2025.
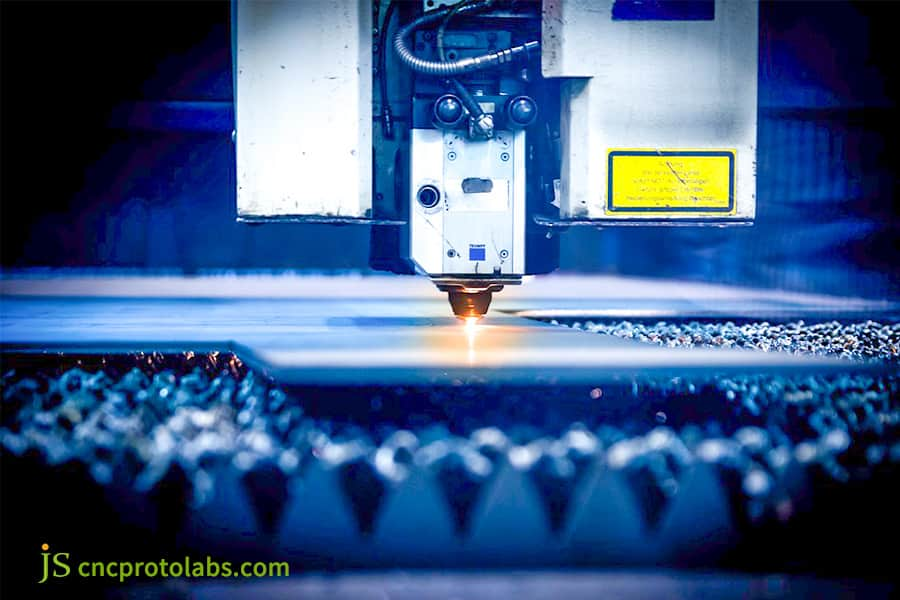
Figure 3: Coaxial nozzle at work on stainless sheet; the supersonic nitrogen jet is what ejects the viscous chromium-rich melt.
What Are the Edge Quality Limits and Break-Even Points of Compressed Air Laser Cutting?
Within custom laser cutting service workflows, compressed air assist cuts hourly gas expenses by 75% for mild steel under 3 mm and unexposed brackets.However, shop air must strictly satisfy ISO 8573-1:2010 Class 1-2-1 filtration with dew points ≤ -40°C. Inadequate oil coalescing allows aerosolized hydrocarbons to contaminate optics under 15 bar, inducing thermal lensing and lens fractures within 100 operating hours.
Cleanroom air compressor purification requirements and hidden cost analysis
- The workshop air compressor must be equipped with a refrigerated dryer and multistage microporous oil-removing filter, with a pressure dew point ≤ -40°C and a remaining oil content ≤ 0.01 mg/m³. Otherwise, oil and water droplets under high pressure will stick to the protective lens when impacted by 15 bar, causing a thermolens effect.
- For custom laser cutting service, although compressed air cutting of 2mm carbon steel can increase line speed with trace amounts of oxygen, a light yellow oxide scale will adhere to the cutting surface.
TCO Accounting and Applicable Boundary Determination
Compressed air cuts assist-gas cost by about 75%, but it relocates the cost rather than removing it: oil and water carry-over at 14–16 bar contaminates the protective window, causing thermal lensing and, if unchecked, lens fracture. Lens replacement therefore belongs in the TCO model, not in the maintenance line item.
Once replacement windows and manual dross removal are priced in, our calibration puts the air-cutting break-even at conventional low-carbon steel up to 3 mm only — and only with ISO 8573-1 Class 1-2-1 purification at a pressure dew point of ≤ −40 °C.
ISO 8573-1:2010, Compressed air — Part 1: Contaminants and purity classes, classifies compressed-air purity as Class [particles]–[water]–[oil]. The practical target here is ISO 8573-1 Class 1-2-1: Class 2 water = pressure dew point ≤ −40 °C, Class 1 oil = ≤ 0.01 mg/m³ — which is exactly what the purification spec below assumes.
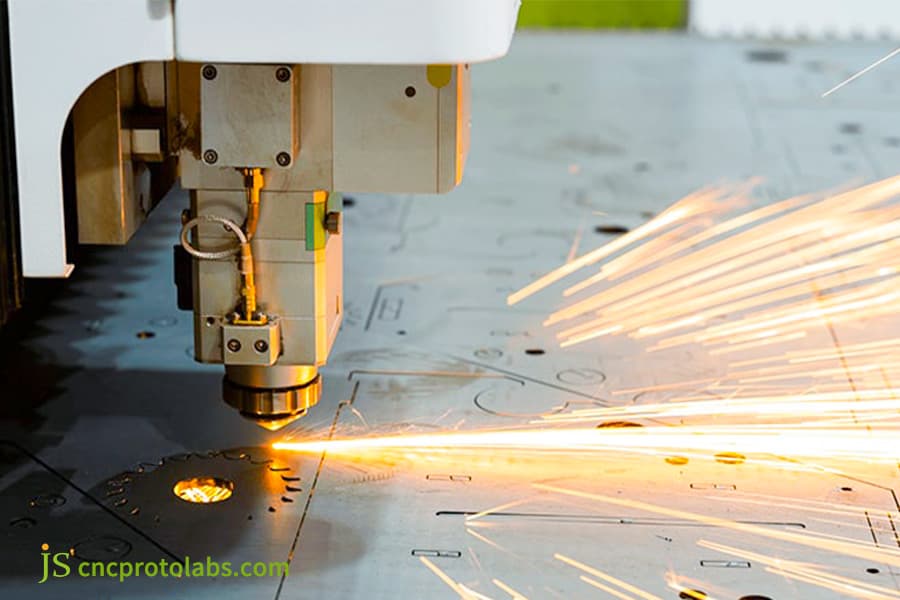
Figure 4: Compressed-air cutting of thin low-carbon sheet — note the brighter, larger spark plume compared with nitrogen cutting.
How Do Laser Cutting Cut Edge Oxide and HAZ Cause Coating Delamination and Weld Defects?
Oxygen-assisted mild steel laser cutting creates a 0.02 to 0.1 mm friable iron-oxide scale alongside a 0.15 to 0.30 mm hardened martensitic edge. Thermal mismatch during 200°C powder curing causes this scale to fracture, failing ASTM D3359 cross-hatch adhesion below grade 2B. Furthermore, rapid edge quenching during laser cutting carbon steel induces moisture entrapment, elevating MIG weld porosity by 40%.
Analysis of Hardened Layer and Welding Defects on the Edge of Carbon Steel Cutting by Oxygen Cutting
- Oxygen cutting of carbon steel results in a 0.15–0.30 mm hardened layer (martensitic structure) formed on the cutting edge which causes a 40% increase in the probability of weld porosity and delayed cold cracking as the weld layer needs manual grind and removal with an angle grinder.
- Based on JS Precision's practical experience in the carbon steel laser cutting project in 2025, switching the 3mm Q235B plate from oxygen to 16 bar nitrogen reduced the coating peeling defect rate from 15% to 0.5%, verifying the decisive impact of gas selection on downstream assembly in laser cutting carbon steel.
Hidden defects in downstream assembly and the choice of overall cost
- A high-pressure nitrogen cut made of stainless steel offers a clean cut surface free of slag and does not damage the original passivation layer. As a result, welding can be done directly with an automatic machine without the need for pickling and passivation which leads to fewer porosities in the welds and a stronger structure, thereby greatly lowering the rates of downstream rework.
- The study revealed through comparison of the failed products that oxy-cutting a carbon steel creates an oxide layer that causes electrocoat paint adhesion failure and decreased strength of structural adhesive bond. The engineer has to make the best decision between gas consumption and future rework/scrap expenses.
How Do You Calculate Laser Cutting Gas Consumption and Cost per Meter?
Estimating cutting assist gas costs within custom laser cutting service requires modeling nozzle expansion dynamics against linear feed rate. In stainless steel laser cutting service on 6 mm plate, an 18 bar nitrogen line through a 2.0 mm nozzle expels 45 to 55 Nm³/h, representing 35% to 45% of running costs. Cryogenic bulk tanks and common-line nesting reduce this consumable expense by 26%.
The three numbers worth memorising. On 6 mm plate over a 1,000 m cut length: oxygen runs about USD 1.20/m but needs oxide removal afterwards; nitrogen on carbon steel runs USD 3.80/m and is powder-coat ready; nitrogen on stainless runs USD 4.50/m and is weld-ready. The gas bill triples between option one and option three — which is precisely why the choice has to be made against the downstream process, not against the gas price.
Fluid mechanics and economic measurement models
- Compressible flow through a constricted nozzle shows a multiplier effect of gas pressure (P) and nozzle cross-sectional area (A) on consumption: at constant pressure, consumption scales close to linearly with orifice area, so a 20% larger orifice costs about 20% more gas. That relationship is the engineering and financial basis of every custom laser cutting service quotation.
- For 6 mm thick stainless steel and nitrogen of 18 bar, the gas consumption is about 45–55 Nm³/h, which is approximately 35%–45% of the operating cost. Make sure to combine power usage and lens wearing in the full cost accounting.
Comparison of comprehensive amortization costs of different gas supply systems
- A 40L high-pressure gas cylinder (15 MPa) is ideal for small-batch prototyping yet the requirement of frequent gas refills leads to more downtime; conversely, a 175L cryogenic liquid nitrogen Dewar (2.8 MPa) can supply a continuous and stable quantity of gas, this way is suitable for a medium-size run, and overall costs would be amortized down by approximately 18%.
- On-site PSA nitrogen generation carries a high capital outlay but the lowest cost per Nm³ once amortised, so it pays back on continuous high-volume lines. Combining it with our common-line nesting and skip-piercing strategy cut total gas consumption by a further 26% on that line.
Comparison Table of Comprehensive Cost Composition for 1000m Cutting Length (6mm Carbon Steel vs 6mm Stainless Steel)
|
Material & Thickness |
Assist Gas |
Avg. Speed (m/min) |
Gas per Meter (Nm³/m) |
Cost per Meter (USD/m) |
Post-Process Benefit |
|---|---|---|---|---|---|
|
6 mm Carbon Steel |
Oxygen (0.6–2.5 bar) |
1.2 |
0.15 |
1.20 |
Requires oxide removal |
|
6 mm Carbon Steel |
Nitrogen (18 bar) |
0.9 |
0.45 |
3.80 |
Powder coat ready |
|
6 mm Stainless Steel |
Nitrogen (18 bar) |
0.8 |
0.55 |
4.50 |
Mirror finish, direct weld |
Data source: JS Precision internal production records, 2025. These are the as-measured cut-quality parameters for each assist-gas / material combination above.

JS Precision Case Study: How Did Gas Optimization Solve Coating Peeling and Kerf Taper on Sheet Metal?
Executing custom laser cutting service on sheet metal enclosures, JS Precision eradicated paint peeling and hinge fitment scrap by re-engineering cutting assist gas parameters. Converting 3 mm Q235B chassis panels from oxygen to 16 bar high-purity nitrogen eliminated friable edge oxidation. For 4 mm 304 stainless hinge brackets, 20 bar nitrogen with negative beam offsets reduced kerf taper to ≤ 0.02 mm, slashing scrap from 18.5% to 0.08%.
Difficulties encountered by customers
- The carbon-steel housing problem. The incumbent supplier cut the full length of 3 mm Q235B plate with oxygen, leaving a hard, brittle iron-oxide layer of about 0.15 mm on the cut face.When the powder coat was cured at 200 °C, differential thermal expansion between the oxide and the steel substrate lifted the coating off in large flakes. The reject rate exceeded 15%, which meant rework on every affected panel.
- The stainless-steel hinge problem. The 4 mm AISI 304 hinge base was cut with 12 bar nitrogen at only 99.5% purity, producing heavy slag on the kerf wall and a 0.1 mm bevelled taper across the cut. The hinge then bound during precision assembly, and overall assembly rejection reached 18.5%.
JS Precision Solution
- Process change for carbon steel. We switched the assist gas from oxygen to a 16 bar N₂ jet on a 12 kW fiber laser, paired with a 1.5 mm single-layer coaxial anti-spatter nozzle. Together these keep the heat-affected zone free of any oxide layer, so the cut face needs no secondary grinding before coating.
- Reset of stainless steel cutting parameters. For the 4 mm 304 hinges we moved to vaporised supply from a centralised 175 L cryogenic Dewar: purity locked at 99.999% (grade 5.0, "5N"), pressure raised to 20 bar, and piercing switched to a three-stage progressive pulse sequence. That combination eliminated spatter blow-back at the pierce point entirely.
- Dynamic optimization of beam focus. The focal position is shifted towards the negative side to one-third below the surface of the plate (-1.5 mm to -2.0 mm), the bottom cut surface is free of slag by the use of supersonic columnar jet effect, and the straight cut verticality deviation is reduced to ≤ 0.02 mm.
Review of failure experiences and lessons learned
During the pilot test of nitrogen cutting carbon steel, the process team initially used the 20 bar high-pressure parameters for stainless steel. The excessively strong cold airflow caused the thin edge of the 3 mm carbon steel plate to warp slightly, triggering two nozzle collision alarms.
Final result
- Quality certification. Parts from JS Precision's custom laser cutting service achieved ASTM D3359 cross-cut rating 5B, with no flaking or blistering after 1,000 hours of neutral salt-spray exposure per ASTM B117. The stainless hinge cuts measured Ra 1.2 μm with a bright silver-white face.
- Mass-production benefit. Holding kerf taper to ≤ 0.02 mm measured across the 4 mm cut height took assembly scrap from 18.5% down to 0.08% and shortened the batch cycle by three working days — removing most of the rework and line-stoppage cost the customer had been carrying.
Need help solving coating delamination or assembly fit failures on cut parts? Contact the JS Precision engineering team and get the same assist-gas optimisation: a parameter set built around your material, thickness and coating spec, so your parts pass salt-spray testing and assemble correctly on the first run.
FAQs
Q1: Why cannot high-pressure nitrogen completely replace oxygen for cutting carbon steel over 10 mm?
Clearing slag from steel above 10 mm with nitrogen requires both high laser power (over 20 kW) and high pressure (about 20 bar). That pushes assist-gas consumption past 90 Nm³/h and raises cost per metre by roughly 300% versus oxygen — consistent with the 8–10 mm and 12–16 mm rows in the table above. Low-pressure oxygen, by contrast, uses the exothermic iron-oxygen reaction to supply 55–65% of the cutting energy and removes slag stably at 1.5–2.5 bar. It also runs faster above 8 mm, which is why thick plate stays an oxygen job.
Q2: How can engineers quickly verify if stainless steel laser cut edges maintain their passivation layer?
- Visual check first. A correct nitrogen cut leaves a uniform silvery-white cross-section with no discolouration. Any yellow or straw tint on the cut face means the assist gas fell below 99.99% purity, or that air was entrained somewhere in the delivery line.
- Confirm chemically if needed. Place one drop of copper sulfate solution on the cut face. Wherever the passive film is damaged, free iron reduces the copper and a visible red copper deposit appears within about 5 seconds — which pinpoints exactly which section of the seam has lost its passivation.
Q3: Why is nitrogen cutting strongly recommended for thin mild steel parts before electro-coating?
Oxygen cutting results in hard, brittle layer of iron oxide that is totally inapt for phosphating and electrophoresis processes. High-pressure nitrogen cutting reveals a pure iron surface, which is able to react with the bath solution to produce a very close protective layer that stops blistering and the peeling of the edges while the material is being used outdoors.
Q4: What is the root cause of frequent laser head protective window failure during compressed air cutting?
The root cause is incomplete purification of moisture and oil mist in the supplied air. Micro-oil droplets in the 16-bar compressed air adhere to the lens, rapidly absorbing heat and carbonizing under laser irradiation, triggering thermal stress that causes the lens to crack. An adsorption dryer with a dew point ≤-40°C must be installed to eliminate this potential hazard.
Q5: Can dross on stainless steel laser cut bottoms be eliminated simply by increasing assist gas pressure?
No. Above about 24 bar the extra pressure stops helping and starts hurting: shock waves and eddies form in the kerf and actually throw more molten burr onto the bottom edge. The effective fix is optical and mechanical instead — move the focus down into the lower third of the sheet and match the nozzle diameter (1.5–2.0 mm) so the flow is genuinely supersonic and stable.
Q6: How does assist gas selection affect hole diameter tolerance in dense sheet metal perforation arrays?
Oxygen is consumed as a reactant, so every pierce injects extra chemical heat into the surrounding material. In dense micro-perforation that heat accumulates and can melt neighbouring hole walls, pushing the array out of tolerance. Nitrogen contributes only momentum and cooling, with no exothermic input, so local heating stays bounded: hole edge shape stays crisp and tolerances hold inside ±0.05 mm even across a dense array.
Q7: How does JS Precision ensure consistent cut edge quality and gas purity in precision laser cutting production?
JS Precision is equipped with a centralized liquid nitrogen storage tank, and the purity of the emitted gas is monitored and locked at over 99.999% online. The machine is equipped with automatic focus calibration and height sensing, and production is controlled according to the ISO 9001:2015 system to ensure consistent surface finish and tolerances for the first piece and mass production deliveries.
Q8: What technical parameters are required to get an accurate laser cutting quote from JS Precision?
Customers only need to provide 2D/3D drawings (DXF, DWG, etc.), specifying the material grade, tolerance accuracy, whether an oxide layer is allowed, and subsequent processes. An engineer will complete the evaluation within 2 hours and return a detailed quotation including gas selection recommendations and quantity calculations.
Summary
Choosing an assist gas for carbon steel and stainless steel is not a consumable decision, it is a process decision. It determines four things at once: the metallographic structure of the cut face, the slag-removal flow field, downstream process yield, and total lifecycle cost.
- Oxygen delivers the fastest throughput on medium and thick carbon steel, using its own exothermic reaction as cutting energy.
- Ultra-high-pressure nitrogen at 99.999%+ purity is the only route to a silver-white, grinding-free, weld-ready stainless edge.
- Compliant compressed air is a genuine cost lever for medium and thin plate, provided the purification meets ISO 8573-1 Class 1-2-1.
Start from the final assembly specification and work backwards to the gas. That is the only reliable way to remove edge delamination and dross before the parts ever reach assembly.
Eliminate cut defects and improve assembly accuracy — starting with the drawing, not the order. Send your engineering drawings to the JS Precision technical team. A senior laser process engineer returns a DFM (Design for Manufacturing) assessment within 2 hours, including the recommended assist gas, expected Ra range, taper expectation, and cost per metre for each option. There is no charge and no obligation: you keep the report whether or not you place the order.
Disclaimer
The contents of this page are for informational purposes only. For JS Precision Services, there are no representations or warranties, express or implied, as to the accuracy, completeness, or validity of the information. It is the buyer's responsibility to identify specific technical requirements and request a formal parts quotation. Please contact us for more information.
Resource

